Batch traceability often breaks after a carton is opened. Parts move into bins, inner bags are discarded, quantities are split, and a new label keeps the part number but loses the original lot. Reliable one-piece fitting batch traceability makes the batch identifier follow the physical fittings through receiving, inspection, repacking, storage, picking, shipment, return, and complaint containment. The objective is not to prove that the parts conform; it is to know which parts share a documented origin and where they went.
Define the Minimum Batch Identity Chain
The chain needs stable identifiers at three levels: the SKU, the batch or lot, and the logistics unit holding the parts. Losing any one makes later investigation slower or impossible.
Connect production identity to received stock
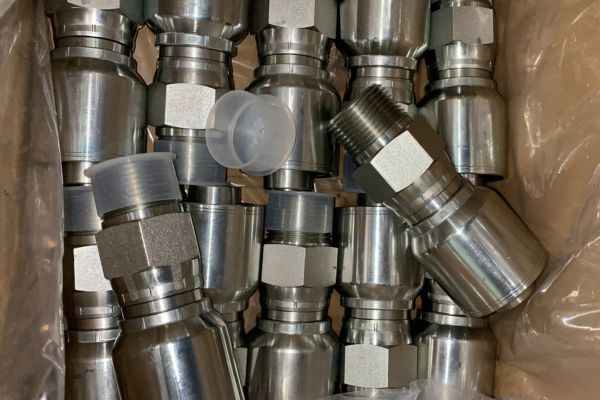
Start with the supplier part number, buyer part number, description, drawing or specification revision where applicable, supplier batch or lot, quantity, purchase order, shipment, and receipt. A batch may represent a production run, material lot, inspection lot, or another defined grouping; document what it means instead of assuming.
The receiving record should show how the supplier identifier maps to the internal item master. If a supplier batch covers several cartons, each carton label should carry or link to that batch. If one carton contains several batches, each inner unit must remain separated and identified.
Give every handling unit a traceable identity
A carton, tote, bin, bag, or pallet may need its own logistics-unit ID in addition to the part and batch. This identifier lets the system record moves and splits without replacing the original batch. Labels should remain legible, securely associated with the contents, and protected from separation.
Do not use location as identity. “Rack A3” tells where stock sits today, not which lot it is. Likewise, a barcode is only useful if the database behind it stores the correct part, batch, quantity, status, and parent-child relationships.
| Process step | Identifier that must survive | Common failure mode |
| Receipt | Supplier SKU, internal SKU, batch, order, quantity | Batch entered in notes but not inventory record |
| Inspection | Sample ID, batch, report, disposition | Results filed without link to held stock |
| Put-away | SKU, batch, status, handling-unit ID, location | Location label replaces original lot label |
| Split or repack | Parent batch and child pack IDs | New bags show part number only |
| Picking and shipment | Picked batch, quantity, shipment or customer order | FIFO used without recording actual lot |
| Return or complaint | Returned item, claimed batch, original shipment | Unverified return mixed into normal stock |
Keep Inner and Outer Labels Linked
Outer cartons support transport and receiving; inner labels preserve identity after the carton disappears. Both should represent the same product and batch without creating competing sources of truth.
Design label hierarchy for opening and splitting
The outer label should show or encode the SKU, batch, quantity, and handling-unit identity required at receipt. Inner bags or subdivisions should carry enough information to remain traceable independently. When a pack is too small for full text, use a durable code linked to a readable system record.
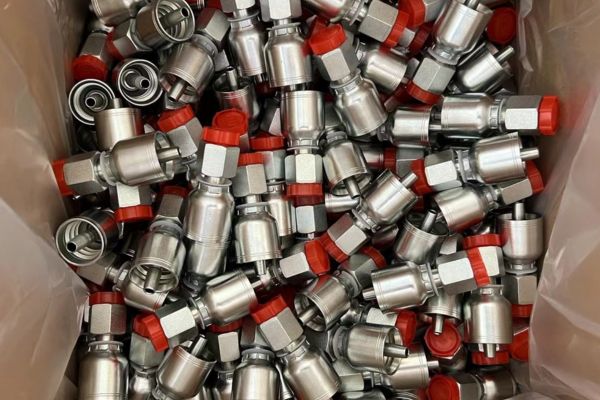
Check label agreement before opening. A mismatch between carton and inner bag requires containment, not a manual correction based on appearance. One-piece fittings can look alike while differing in thread, seat, port dash, hose dash, orientation, material, or finish.
Preserve the original evidence
Do not discard every supplier label as soon as stock is received. Retain label images or source records according to the document policy, especially when internal relabeling occurs. Record who created the internal label, when, from which original unit, and in what quantity.
Handwritten corrections need control. Crossing out a batch and writing another without a logged reason destroys confidence in the chain. Use a defined relabel transaction that leaves the original value, new value, reason, user, and time available for review.
Link Receiving and Inspection Records to the Lot
Receiving creates inventory identity; inspection establishes status for the sampled lot. The two records should connect without relying on filenames or personal memory.
Capture batch before samples leave the carton
At receipt, verify labels, count, packaging condition, SKU, batch, and order. Assign a receipt or handling-unit ID and photograph discrepancies before moving parts. Samples sent to inspection should retain a sample ID tied to the parent batch and unit.
The inspection report should reference part number, batch, drawing or requirement revision, sampled quantity, characteristics, results, disposition, and report ID. Stock in quarantine should carry the same identifiers. A report marked “pass” is useless if staff cannot determine which physical bins it released.
Keep status distinct from batch identity
Accepted, quarantined, rejected, and awaiting-review parts can share a batch number. Status indicates disposition; batch indicates origin. Never alter the lot value to represent quality status, and never assume a known batch is conforming merely because it is traceable.
When only part of a batch is inspected or reworked, create controlled sublots if the quality procedure requires them. Record the relationship to the parent batch, affected quantity, operation, date, and new status. Avoid silently returning corrected parts to the original bin.
Control Stock Splits and Repacking
Repacking is the highest-risk moment because a single labeled unit becomes several smaller units. The process must create children that inherit identity without allowing quantities or batches to drift.
Use a parent-child transaction
Scan or enter the parent handling unit, verify SKU and batch, state the quantity removed, and create child pack IDs. Each child label should include the same batch plus its quantity and unique pack identity. The system should reduce the parent’s balance and preserve the total.
Perform one SKU and one batch at a controlled station whenever practical. Clear previous labels and loose parts before starting. If two lots of the same SKU are open nearby, physical appearance cannot protect against mixing. Use separate zones, containers, and transaction completion before opening the next lot.
Stop when identity is missing
An unlabeled bag should enter an unknown-status location, not receive the nearest likely batch. Compare purchase, receipt, inspection, count, and packaging evidence to investigate, but do not reconstruct a lot from appearance alone. If identity cannot be demonstrated, manage the parts as untraceable under the approved disposition.
Never pour an unknown quantity into traceable stock to “make the count right.” That action contaminates the identity of the entire bin and expands future containment from one bag to all potentially mixed inventory.
Carry Batch Data Through Warehouse Moves
Warehouse transactions should move a specific SKU, batch, status, handling unit, and quantity from one location to another. Recording only the item and location loses the information needed for containment.
Keep physical and digital stock synchronized
Scan the source unit, destination, and quantity at the time of movement. Avoid paper notes that are entered later after several bins have moved. Cycle counts should compare not only total quantity but quantity by batch and status.
Bins with fixed SKU labels still need variable batch identification. If mixed batches are permitted in one location, use separate inner units and system records; do not combine loose parts. Where the system cannot track multiple lots in one bin reliably, use one batch per location.
Handle picking without hiding the lot
FIFO or FEFO logic can choose a lot, but the actual picked unit must be recorded. Substitution at the shelf, short picks, and partial packs should update the batch and quantity before shipment. A packing slip that lists only the part number cannot recreate the actual lot later.
For kits or hose assemblies, record which fitting batch entered the finished item when required by the traceability plan. The parent assembly ID can link component batches without printing every code on the final product, provided the digital relationship remains retrievable.
Link Outbound Shipments and Returns
Traceability reaches its business value when a team can answer which customer or internal job received an affected batch and which batches may have produced a complaint.
Record the actual shipped batch
Connect shipment, order line, SKU, batch, quantity, handling-unit IDs, date, and destination. Retain packing and label evidence according to policy. If the customer needs batch data on documents or labels, define the format before shipment.
When an order draws from more than one batch, list each quantity separately. Do not collapse them into a single invented lot. This precision allows narrow containment and avoids contacting customers who received unaffected stock.
Quarantine returns until identity is verified
A returned fitting may carry a label, customer statement, original carton, or no reliable identity. Link it to the original shipment using order, item, batch, quantity, and photos. Customer-provided batch information is useful evidence but should be verified against outbound records.
Do not mix returns into saleable stock, even when unused. Preserve damage, packaging, and labels for investigation. If the batch cannot be confirmed, record it as unknown and keep its conclusions separate from verified-lot analysis.
Use Traceability for Complaint Containment
Traceability shortens the path from a reported part to potentially affected inventory and shipments. It does not prove the cause or imply that every item in the lot is defective.
Trace backward and forward
Backward tracing identifies the receipt, supplier batch, material or process records, inspection, repacks, and parent units associated with the complaint. Forward tracing identifies remaining locations, child packs, internal jobs, assemblies, and outbound shipments.
Define the containment boundary from available evidence. It may begin with one verified batch and expand if labels, process history, or mixed stock make the boundary uncertain. Record why the scope was chosen and what information remains unverified.
Test retrieval before a real complaint
Run periodic trace exercises using a selected shipped unit. Ask the team to retrieve its receipt, batch, inspection, current inventory, repack history, and destinations within the organization’s target time. Measure missing links and correct the process.
A successful software query is not enough if the physical bin contains mixed or unlabeled parts. The exercise should compare digital records with labels and stock. Traceability is a chain of custody across both domains.
Follow a Physical-to-Digital Workflow
Implementation succeeds when each physical action has a small, mandatory transaction and an exception path. Complex software cannot rescue uncontrolled relabeling at the bench.
Operational sequence
- Verify supplier SKU, internal SKU, batch, quantity, order, and label agreement at receipt.
- Assign a receipt and handling-unit ID without replacing the original lot.
- Link samples, inspection reports, status, and disposition to the physical units.
- Put away stock by SKU, batch, status, unit, quantity, and location.
- During every split, create labeled child units linked to the parent and reconcile quantities.
- Record each move and pick using the actual handling unit and batch.
- Link shipped batch quantities to the order, destination, and packing record.
- Quarantine returns and unknown labels until identity is verified or formally dispositioned.
- Use backward and forward queries for complaints, then confirm records against physical stock.
Exception handling is part of the workflow. Define where unknown, damaged-label, mixed, excess, short, and returned stock goes, who may resolve it, and what evidence is required. Without an exception path, operators will create unofficial labels to keep work moving.
Conclusion
Batch identity must stay attached to the parts after the original carton is gone. Build the chain from supplier lot and received SKU through handling units, inspection, status, repacking, locations, picks, shipments, and returns. Parent-child transactions preserve identity during splits, while controlled exception locations prevent unknown stock from contaminating traceable bins. Digital records and physical labels must agree; neither can substitute for the other. A retrieval chain should be narrow enough to act on and complete enough to defend. Because traceability supports identification and containment rather than proving conformity, keep quality status and lot identity separate. Before relying on one-piece fitting batch traceability, test backward and forward retrieval, reconcile quantities, inspect physical labels, and close every missing or mixed-batch exception.
Frequently Asked Questions
Can two batches of the same fitting share one bin?
Only if the system and physical controls keep them in separate labeled units and can track each quantity reliably. Otherwise, use separate locations to prevent mixing.
What should happen when fittings are repacked?
Create child pack IDs that inherit the parent batch, record transferred quantities, and label every child before it leaves the controlled station. Preserve the parent-child transaction.
Can a missing batch label be recreated from appearance?
No. Investigate receiving, order, count, and packaging evidence, but manage the stock as unknown unless the original batch link can be demonstrated.
How should customer returns be traced?
Quarantine the return and link it to the original shipment using order, SKU, batch, quantity, labels, and photos. Do not mix it into saleable inventory.
Are digital records enough for batch traceability?
No. The database must agree with physical labels, contents, status, quantities, and locations. Periodic trace exercises should verify both sides of the chain.