You should buy hydraulic hose and fittings from the same supplier when that arrangement gives your recurring assembly program a clearer approved combination, stronger document control, and simpler responsibility—but common supply alone does not prove compatibility. Separate sourcing can work when every hose, fitting, ferrule, crimp specification, tool, and inspection requirement is independently approved and controlled. The wrong decision creates more than purchasing inconvenience: it can produce unapproved assemblies, conflicting revisions, unclear failure ownership, and repeated order errors.
Start With the Combination, Not the Supplier Count
The first question is whether the exact hose-and-fitting combination is technically approved for the intended assembly process. A single supplier may sell both categories without documenting that a particular hose series, fitting series, ferrule, crimper, die set, and crimp instruction belong together. Two suppliers may provide a valid combination only when an approved system owner or competent engineering process establishes and controls it.
What approval must identify
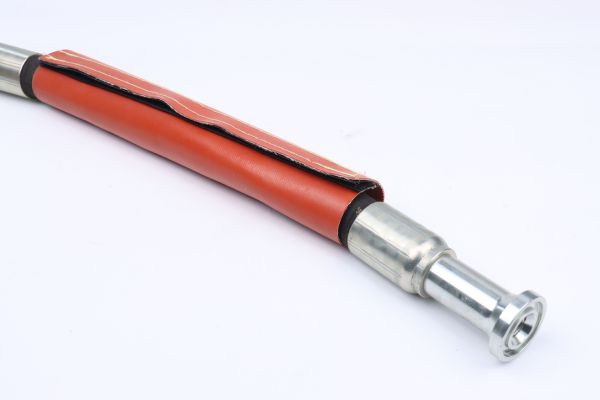
The record should name the hose manufacturer and series, hose size and construction, fitting and ferrule series, applicable crimp machine and tooling, preparation method, insertion requirement, crimp specification, and inspection criteria. It should also state the document revision and application limits that matter, including fluid, temperature, pressure duty, routing, and any equipment requirements. A generic statement that products are “compatible” is not a substitute for this combination-level evidence.
Do not infer approval from matching dash sizes, similar stem geometry, shared branding, or successful assembly by feel. These clues may narrow a search but cannot reveal how hose construction, ferrule compression, stem engagement, and finished crimp behavior interact. The applicable current data must control the assembly.
Same supplier is evidence only when documented
Coordinated supply can make evidence easier to obtain because one commercial channel may provide the hose, fitting, and current assembly data. That benefit exists only if the documents are specific, current, and traceable to what is shipped. A supplier relationship does not turn an undocumented combination into an approved one.
Compare Technical Control in Each Sourcing Model
Technical control is usually simpler when one documented system covers the combination, but separate sourcing can be equally disciplined with a defined approval owner. The practical difference is the number of interfaces that must be reconciled and maintained. More interfaces increase administrative work even if they do not automatically increase technical risk.
Coordinated supply
Under coordinated supply, the purchase description can reference one approved combination list and one revision-controlled assembly instruction. Product substitutions, phase-outs, and document changes may be easier to detect when the supplier is responsible for presenting the complete proposed system. Incoming records can also use aligned part identifiers and packaging labels.
However, the buyer must still verify that the delivered hose and fittings match the referenced series and revisions. A supplier might offer several families that are not cross-compatible, or supply a hose and fitting as separate catalog items without approving their use together. The assembly team remains responsible for following the correct procedure and inspecting the result.
Separate sourcing
Separate sourcing gives buyers flexibility to manage availability, commercial terms, and category expertise independently. It also creates a technical integration task: someone must maintain the approved cross-supplier combination, monitor both product revisions, resolve conflicting instructions, and control substitutions. If no one owns that integration, the purchasing model is incomplete.
Mixed-brand or cross-source assembly should never be justified by apparent fit or an old workshop habit. Approval needs valid engineering or manufacturer evidence for the exact combination and process. When that evidence is unavailable, buy the components separately only for uses that do not imply unapproved assembly, or pause the decision for technical review.
Documentation and Responsibility Decide Repeatability
Recurring programs depend on records that survive staff changes, repeat orders, and product revisions. The sourcing model should make it obvious who owns the bill of material, approval basis, crimp data, deviation review, incoming inspection, assembly record, and nonconformity response. Unclear responsibility is a predictable source of inconsistent assemblies.
Build a responsibility matrix
Assign one accountable owner for each control rather than relying on informal cooperation. Purchasing can confirm the commercial item and revision requested; engineering or the system owner can approve the combination; quality can define receiving and assembly records; production can follow the controlled work instruction. Suppliers provide requested evidence, but the buyer still decides whether it satisfies the program.
At minimum, assign responsibility for:
- Maintaining the approved hose, fitting, ferrule, and tooling combination list
- Obtaining and distributing current crimp specifications and assembly instructions
- Reviewing substitutions, obsolete parts, and conflicting revisions before use
- Linking received lots to purchase descriptions and assembly records
- Controlling crimper settings, dies, calibration, inspection, and operator authorization
- Investigating nonconformities without assuming which supplier caused the problem
With one supplier, several evidence requests may go through one contact, but internal ownership still matters. With separate suppliers, the matrix needs an explicit integration owner who can see both sides of the assembly.
Commercial Workflow Can Favor Either Choice
Once technical approval is protected, compare order administration, freight, lead-time exposure, inventory, and service continuity. These factors affect total workload and availability, but they should not override the approved combination. A cheaper or faster component is not useful if it cannot be assembled under controlled data.
Order and freight coordination
One supplier can consolidate purchase orders, shipment tracking, documentation requests, and sometimes freight. This may reduce administrative handoffs and mismatched arrival dates. The actual benefit depends on origin, product availability, shipment terms, consolidation practices, and whether combining goods creates a delay for the complete order.
Separate sourcing can allow each category to follow its best replenishment pattern. It may also split freight, customs documents, minimum order constraints, payment workflows, and delivery tracking. Buyers should compare the real landed workflow rather than assume one shipment is always cheaper or two suppliers are always more resilient.
Continuity and concentration
Single-source coordination may simplify repeat orders but can concentrate disruption risk. Separate sourcing may diversify supply, yet it can also create dependence on a narrow approved cross-source combination that becomes invalid if either component changes. Resilience comes from approved alternatives, controlled inventory, and change monitoring—not merely from counting supplier names.
Use a Decision Matrix for the Program
Score each sourcing model against evidence and workload that can be observed. Do not assign universal weights; the program owner should decide which criteria matter most for the assembly mix and service requirement. A safety-critical combination may place technical control above every commercial convenience.
| Decision criterion | Same-supplier model | Separate-supplier model | Evidence to request |
| Combination approval | May be easier to obtain, but must be explicit | Requires an identified integration and approval basis | Exact combination list and revision |
| Crimp and assembly data | Potentially aligned through one system | Must reconcile sources and control one approved instruction | Current crimp sheet and tool requirements |
| Change notification | One channel may coordinate changes | Both component changes must be monitored | Change-control commitment and affected-part review |
| Order administration | Fewer purchase and document handoffs | Category orders can be optimized independently | Process map, order records, document workload |
| Freight and delivery | Consolidation may help or delay the full order | Split delivery may improve flexibility or add cost | Actual routes, terms, schedules, and landed cost inputs |
| Responsibility | Commercial contact may be clearer | Integration owner must be explicit | Responsibility matrix and escalation path |
| Continuity | Concentrated source exposure | More sources, but combination dependency remains | Approved alternatives and inventory plan |
| Nonconformity review | One supplier can coordinate evidence | Evidence must be collected from both sources | Lot traceability and investigation procedure |
A Clearly Hypothetical Comparison
Consider a hypothetical business with a recurring family of hose assemblies. Option A offers hose and fittings through one supplier, plus a current combination list and a controlled crimp-data source. Option B uses separate suppliers; both provide detailed component records, but the buyer has not yet established who approves the combined assembly or monitors revision changes.
How the decision should proceed
Option A has a documentation advantage, but it is not automatically selected. The team verifies that the proposed hose and fitting part numbers actually appear together in the approved data, that its crimper and dies are covered, and that the application falls within the stated limits. It then checks order terms, availability, freight, and change control.
Option B remains viable if the team obtains a valid combination approval and assigns an integration owner. Without that evidence, a lower unit price or better component availability cannot justify assembly. The team may request a documented technical review, limit Option B to separately approved uses, or keep it as an unapproved commercial alternative rather than silently releasing it to production.
This example contains no assumed product performance, supplier capability, or savings. Its purpose is to show that the missing approval owner—not the number of suppliers—is the decisive gap.
Gather Comparable Inputs Before Choosing
Each proposal should answer the same technical and commercial questions. If one quote contains a complete system and the other lists unrelated components, they are not yet comparable. Normalize the scope before evaluating price or workflow.
Required evidence package
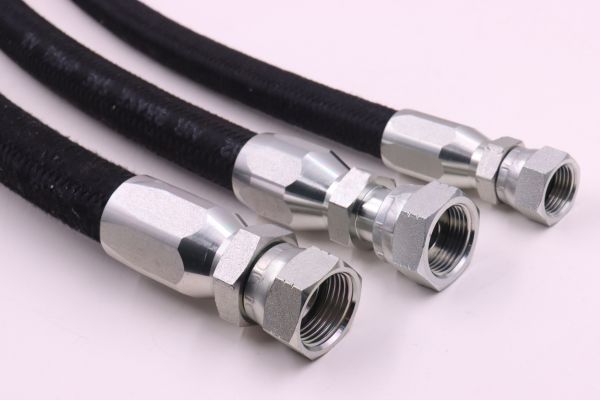
Request the following for the exact proposed products:
- Hose and fitting part numbers, descriptions, sizes, series, materials, and revision status
- Combination approval source and current assembly/crimp instructions
- Crimper, die, tooling, preparation, insertion, and finished-inspection requirements
- Lot identification, certificates or conformity records required by the program
- Substitution and product-change process, including notification and approval ownership
- Ordering units, packaging quantities, lead-time basis, shipment terms, freight inputs, and document fees where applicable
- Nonconformity contact path and evidence expected from buyer and supplier
Keep product-specific performance claims with their source. Do not transfer an approval from a supplier’s other hose, fitting family, size, market, or test program to the proposed combination.
Avoid Common Purchasing Mistakes
The most common mistake is treating convenience as compatibility. Others include accepting a verbal mixed-brand assurance, using obsolete crimp sheets, comparing unit prices without assembly labor and documentation workload, or assuming separate suppliers automatically provide resilience. These errors obscure the actual cost and risk of maintaining a repeatable program.
Final decision checklist
Before release, confirm that one controlled record names the approved hose, fitting, ferrule, tooling, and procedure. Confirm who monitors changes, who can approve deviations, and how received lots connect to finished assembly records. Then compare commercial inputs using the same scope and period.
Choose the same-supplier model when its documented combination and coordinated workflow materially reduce control burden without creating unacceptable concentration. Choose separate sourcing when the combination is independently approved, integration ownership is strong, and the availability or commercial benefits justify the extra interfaces. If technical evidence is incomplete, the correct decision is to pause—not to select the more convenient quote.
Conclusion
Buying hydraulic hose and fittings from the same supplier can simplify combination records, change communication, freight, and order administration, but shared supply is not technical approval. Separate sourcing can be reliable when the exact hose, fitting, ferrule, crimper, tooling, and crimp specification are approved together and one owner controls revisions and deviations. Compare both models with the same evidence package, responsibility matrix, landed workflow, and continuity assumptions. Do not use matching dash sizes, visual fit, unit price, or supplier count as proof of a safe assembly. The practical next step is to document the proposed combinations and identify every missing approval before commercial comparison. That evidence—not organizational convenience—should determine whether to buy hydraulic hose and fittings from the same supplier.
Frequently Asked Questions
Does one invoice prove the hose and fittings are compatible?
No, one invoice proves only that the items were sold through one commercial channel. Compatibility requires current, combination-specific technical data covering the exact components and assembly process.
Can separate suppliers share responsibility for an assembly failure?
Responsibility depends on contracts, evidence, and the actual cause, so it should not be assumed in advance. Define technical integration, records, investigation duties, and escalation paths before production.
Should freight savings decide the sourcing model?
No, freight is one commercial input after technical approval has been secured. Compare actual landed workflows, because consolidation can either reduce handoffs or delay a complete order.
Is a second supplier always a better continuity plan?
No, a second supplier improves continuity only when its products and combinations are approved and can be controlled. An unapproved alternative adds a name to the supplier list without creating usable capacity.
What record is most important for repeat orders?
The most important record is the current approved combination and assembly specification linked to exact part numbers and revisions. Purchase, lot, tooling, inspection, and change records should all point back to it.